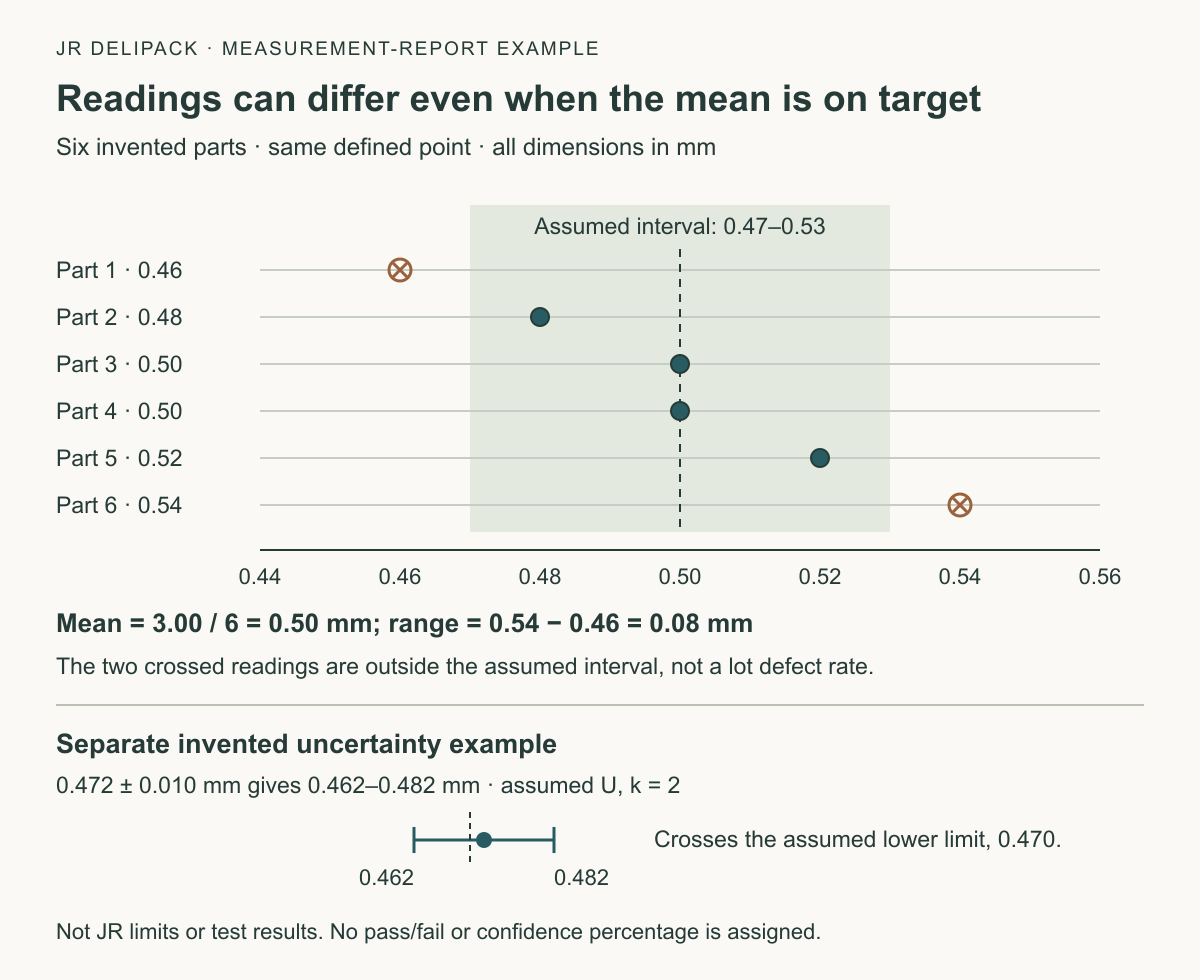
Ask for a PP container wall-thickness report tied to defined measurement points, limits and a method—not just an average: six hypothetical readings at the same point on six separate containers can average 0.50 mm while two readings fall outside an assumed 0.47–0.53 mm interval. The calculation below shows why a summary number is not a complete purchasing decision.
This guide explains how to request and review that report. Its numerical examples are invented for procurement training, not JR DELIPACK specifications, production measurements or recommended tolerances. A measurement report should make the supplied evidence understandable; it does not by itself establish lid fit, food-contact suitability or acceptance of an entire delivery.
What should a supplier's thickness report identify?
Start with the exact container or component, not a product-family nickname. Record the model, material identification, drawing revision and production or sample reference. State whether the report concerns the base, lid or another component. An invoice description can remain commercially useful without being precise enough to identify a measurement location.
Ask for the target and permitted limits at each required location, the individual readings, the units, the measurement method and the sample-selection record. Also request the report date and the person or laboratory responsible. If a supplier cannot provide a field at quotation stage, mark it unresolved and agree when it will be supplied. Do not replace a missing measurement with a catalogue description.
Distinguish the drawing's intended dimensions from measured results. A value copied from a specification belongs in a target column; it should not appear as though someone measured every sample at that exact value. Similarly, a report covering development samples should retain that description rather than becoming a production-lot certificate when forwarded internally.
For your purchasing file, use a compact report cover sheet:
| Field | Proposed buyer request | Reason for keeping it |
|---|---|---|
| Product and revision | Exact component and controlled drawing | Links the report to the ordered article |
| Point map | Named locations with dimensions or annotated images | Makes repeat measurements comparable |
| Specification | Target and limits for each location, with units | Separates requirements from observations |
| Method | Instrument, contact arrangement and preparation | Identifies how readings were obtained |
| Sample identity | Part identifiers and selection record | Shows the population actually examined |
| Results | Individual readings, summary and limitations | Avoids relying on an unexplained average |
| Decision | Agreed rule and named reviewer | Separates measurement from purchasing approval |
How do you define locations without mixing different questions?
Use an annotated drawing or sample image that both parties can interpret. A description such as “sidewall” may need an orientation, distance from a reference feature and clarification of whether a rib or embossed area is included. Give each location a stable identifier. Avoid changing those identifiers between a quotation sample and a delivery inspection.
Keep two questions separate. Measuring different positions on one container describes that part's distribution of thickness. Measuring the same defined position across several containers describes the observed variation between those sampled parts. Combining both into one average can hide which question the result answers. Use separate rows for location and separate columns or records for individual parts.
For example, call an agreed sidewall location S1 and a base location B1. If their approved targets differ, calculate each location's summary against its own requirement. Do not average S1 and B1 together and compare the result with the S1 limit. This is a proposed reporting convention, not a prescribed design for a JR container.
Also distinguish component geometry from the chosen measurement standard. ISO 4593:1993 describes mechanical thickness measurement for plastics film and sheeting; its public scope excludes embossed film or sheeting. That scope does not automatically establish a suitable method for every finished container location. 1: ISO film and sheeting method scope (reference details).
If a supplier cites a standard, ask which provisions and preparation steps apply to the actual geometry. Have the responsible technical reviewer resolve any adaptation rather than recording the standard number alone as proof. The public scope is a useful screening reference, not a substitute for the complete method where that method is required.
What does the worked example reveal that an average hides?
Assume six separate containers were measured at the same location using the same agreed method. The invented readings are 0.46, 0.48, 0.50, 0.50, 0.52 and 0.54 mm. Assume, only for this example, a nominal target of 0.50 mm with a tolerance of ±0.03 mm, giving lower and upper limits of 0.47 and 0.53 mm.
The readings sum to 3.00 mm. Dividing by six gives a mean of 0.50 mm, exactly the assumed nominal target. Yet the lowest reading is below the lower limit and the highest is above the upper limit. The observed range is 0.54 minus 0.46, or 0.08 mm. Reporting only the mean would conceal both observations.
| Part identifier | Hypothetical S1 reading | Numerical comparison with assumed limits |
|---|---|---|
| A | 0.46 mm | Below 0.47 mm |
| B | 0.48 mm | Within interval |
| C | 0.50 mm | Within interval |
| D | 0.50 mm | Within interval |
| E | 0.52 mm | Within interval |
| F | 0.54 mm | Above 0.53 mm |
These comparisons intentionally leave out measurement uncertainty and the contractual decision rule, addressed below. They are not a declaration that the production lot must be rejected. Six example readings do not establish the delivery's defect rate, its worst possible thickness or a statistically justified sampling plan. Do not multiply the two observations into an estimated quantity of defective cartons.
For a real report, keep the original readings and ask the reviewer to investigate the affected locations and sample identities. If only an average was supplied, request the underlying records before comparing suppliers. Do not invent individual readings that would reproduce the average: several different datasets could produce the same summary.
Which measurement details make supplier and buyer results comparable?
Request the instrument type and identifier, its reporting resolution, the contact arrangement, any fixture and the preparation method. Ask whether measurements were made on an intact part or a prepared section. If preparation is destructive, record which samples were consumed and retain their identification. A receiving team should not unknowingly compare intact-part readings with a different sectioning method.
Have the technical reviewer define suitable contact geometry, force, orientation and handling for the part rather than copying generic settings from this article. Document relevant conditioning and measurement conditions where the chosen method requires them. The aim is a repeatable instruction that the actual teams can follow, not the most elaborate equipment list.
Calibration information belongs in that record, but a calibration sticker is not a full explanation of the measurement result. NIST explains that metrological traceability concerns a result supported by a documented calibration chain; use of a calibrated instrument alone is insufficient. It also distinguishes traceability from fitness for the user's particular measurement need. 2: NIST traceability and fitness for purpose (reference details).
Before arguing that one supplier's product differs from another's, check whether the measurement processes are comparable. Where results are disputed, agree a shared sample identification and a controlled comparison, retaining both sets of observations. A gauge study can contribute to uncertainty assessment when it represents the working measurement process; NIST warns that changed process characteristics can undermine that assessment. 3: NIST gauge-study uncertainty guidance (reference details).
Do not keep measuring until a preferred number appears. Record repeat measurements as additional observations with their reason, not replacements for inconvenient originals. If an instrument or procedure is changed during investigation, distinguish the new series so the reviewer can decide whether comparison is valid.
How should tolerance, resolution and uncertainty affect the decision?
Keep specification limits separate from the information describing a measurement. In the example, the permitted interval is an invented purchasing requirement. Instrument resolution describes a reporting increment; it should not be silently used as the tolerance or treated as a complete uncertainty statement. Ask the measurement provider to identify the uncertainty information appropriate to the result and its intended use.
NIST Technical Note 1297's reporting guidance distinguishes combined standard uncertainty from expanded uncertainty and calls for the coverage factor when expanded uncertainty is reported. It cautions against automatically assigning a confidence interpretation without an adequate basis. The note is historical measurement guidance, not a packaging specification or a current approval rule for JR products. 4: NIST reporting uncertainty guidance (reference details).
Consider another explicitly hypothetical result: 0.472 mm, with assumed expanded uncertainty U = 0.010 mm and an assumed reported coverage factor k = 2. The interval formed by subtracting and adding U is 0.462–0.482 mm. It crosses the earlier assumed lower specification limit of 0.470 mm, even though the reported central value is above it.
That illustration is not automatically a pass or failure, and no confidence percentage is asserted for it. The purchasing agreement needs a documented decision rule explaining how uncertainty is handled, who reviews borderline results and what happens while the decision remains open. Have qualified measurement personnel establish the real uncertainty and rule; neither may be inferred from this invented example.
Agree how rounding is handled as well. Preserve the recorded precision and avoid silently rounding a near-limit result into apparent conformity. If two reports use different displayed precision, obtain the underlying records and measurement explanations rather than treating the number of printed decimal places as evidence of greater accuracy.
How do sample results relate to the shipment?
Identify the lot or sample population, how parts were selected and the production coverage available in the record. Where cavity or production-period information exists and is relevant, retain it. If it is unavailable, describe the limitation. Do not imply that a few individually selected samples represent every cavity or the complete order.
Ask the responsible quality parties to agree the sampling and disposition approach before inspection. ISO 2859-1:2026 describes AQL-indexed acceptance sampling by attributes for lot-by-lot inspection. Its public abstract does not supply a bespoke sample size or acceptance decision for your wall-thickness programme. No sampling tables from the standard are reproduced here. 5: ISO acceptance-sampling scope (reference details).
A numerical thickness report and an attribute-based acceptance decision are related records, not interchangeable labels. If measured results are converted into conforming or nonconforming classifications, retain the specification, measurement decision rule and sampling plan that produced those classifications. A report marked “AQL checked” without those connections is not enough to reconstruct what was inspected.
Separate sample approval from routine production verification. The former records what was reviewed for the proposed configuration; the latter needs evidence tied to the delivered material. Reusing a sample report may help explain the specification, but it should not be relabelled as a fresh inspection of an unexamined delivery.
What should purchasing do when the report is incomplete?
Send a specific clarification request: name the missing point map, revision, readings or method detail and explain the decision it prevents. Assign a person responsible for obtaining the answer and a person authorised to review it. This keeps a documentation issue from disappearing inside a general request for “better quality.”
Distinguish a missing record from a demonstrated dimensional discrepancy. Both may require action, but the actions differ. A missing map may need clarification and matched remeasurement; an identified out-of-limit reading may need investigation under the agreed quality process. Preserve the initial report, the clarification and the resulting disposition together.
If two supplier offers report different locations, ask for a common comparison basis before ranking them by thickness. The comparison should also identify what the quotation includes: measurement scope, report timing and any separate inspection arrangement. Do not assume a report or independent inspection is included merely because a seller answered a technical question during enquiry.
For reorder control, record changes to the drawing, material identification, tooling or method and ask whether they affect comparability with the approved baseline. This is a proposed change-review process, not a claim that every change requires the same test or automatically causes failure. Keep superseded records identifiable instead of overwriting their dates.
What else belongs beside the thickness report?
Retain the report alongside dimensions, the agreed packaging configuration, application requirements and relevant functional evidence. A dimensional observation should not be converted into an unsupported promise of leak resistance, microwave suitability, load capacity or food-contact compliance. Request the appropriate product-specific evidence for each separate question you actually need answered.
For the distinct task of assessing a matched base and lid, use the container-and-lid purchasing checklist. Keep its observations in a separate section of the buying file, linked by component identity. That makes it possible to review both records without allowing one to stand in for the other.
JR DELIPACK supplies PP, PLA and paper-based foodservice packaging with supply and manufacturing support. Explore the product range and factory and quality information when preparing an enquiry. Availability of measurements and supporting records must be confirmed for the particular product and proposed order.
Frequently asked questions
Can I ask for one wall-thickness figure?
Yes, if the figure is clearly a nominal target for a defined location or another expressly defined summary. Request its scope and the underlying measurement record. A single number should not be presented as though it describes every point, every sampled part and every unit in the shipment.
Does an average at the nominal target mean the samples meet the limits?
No. The hypothetical example has an average at the target while individual readings sit outside the assumed interval. Review individual observations by location, then apply the agreed uncertainty and decision rules. Do not turn a summary statistic into a shipment acceptance statement without that process.
What if the buyer and supplier obtain different results?
First compare sample identity, location, revision, preparation and measurement method. Retain both reports and document any controlled repeat work. If the disagreement persists, use the agreed technical escalation or independent evaluation arrangement; repeatedly selecting the more favourable reading does not resolve the discrepancy.
Is a thicker container automatically a better purchase?
Do not make that assumption. Define the application and evaluate the exact configuration against its requirements. This guide offers no universal thickness recommendation, and a higher thickness figure does not itself document the pack's other performance or suitability claims. Compare evidence for the purchasing task, not an isolated marketing number.
Can a supplier keep its drawing confidential?
Arrange the technical detail needed for an agreed review through an appropriate private channel. A controlled point map or another agreed record may resolve the reporting question without publishing proprietary drawings. Lack of public disclosure is not itself evidence of poor quality, but the buyer still needs sufficient information to evaluate the report.
When should the report be reviewed again?
Follow the agreed inspection plan and change-review process. Review whether later deliveries and revised configurations remain covered by the existing records. Do not invent a universal retest interval from this article; document the actual triggers, responsibilities and evidence required for your purchasing programme.
Prepare a specific enquiry
Contact JR DELIPACK with the container reference, intended application, destination, quantity and the measurement question you need answered. Include a permitted drawing or point map through an appropriate private channel. Ask which reporting scope can be supported for the proposed order rather than assuming this guide is a product test record.
References
- ISO. ISO 4593:1993, public scope for thickness measurement of plastics film and sheeting. Second edition, 1993. Public informative sections reviewed; complete paid standard not reviewed. Accessed 6 October 2026. Return to discussion.
- NIST. Metrological Traceability: Frequently Asked Questions and NIST Policy. Page created 29 April 2010; updated 27 May 2026. Policy and measurement-result/fitness-for-purpose discussion reviewed. Accessed 6 October 2026. Return to discussion.
- NIST/SEMATECH e-Handbook. Section 2.4.6: Quantifying uncertainties from a gauge study. Publication date not displayed on the reviewed section. Accessed 6 October 2026. Return to discussion.
- NIST. Technical Note 1297, section 7: Reporting Uncertainty. Technical note edition 1994; web page created 6 November 2015 and updated 3 June 2026. The page carries a notice that it is no longer updated; used here for historical reporting principles, not a current packaging requirement. Accessed 6 October 2026. Return to discussion.
- ISO. ISO 2859-1:2026, public acceptance-sampling abstract. Third edition, published January 2026. Public scope only; complete paid standard and sampling tables not reviewed. Accessed 6 October 2026. Return to discussion.
“How Suppliers Report Wall Thickness on PP Containers”的一个回复